Top Compressed Air Systems for Global Buyers
Global manufacturers need compressed air systems that deliver stable pressure, efficient operation, and dependable service across demanding production environments. A system may look simple: compressor, receiver, dryer, filters, and distribution piping. In practice, every component affects product quality and operating cost. A pressure drop at the farthest workstation can interrupt packaging, machining, or automated assembly. Small details matter.
The U.S. Department of Energy reports that compressed air can represent roughly 10% of industrial electricity use. Its compressed air guidance also indicates that leaks may waste 20% to 30% of compressor output. Those figures explain why global buyers should assess total cost of ownership, not only purchase price. The International Energy Agency continues to identify industrial efficiency as a major pathway for reducing energy demand and emissions. However, efficiency claims need verification. Always request measured flow, pressure, specific power, and sound-level data.
This guide examines top compressed air systems for global buyers, including oil-free and lubricated designs, variable-speed compressors, modular packages, and integrated treatment equipment. It considers factory climate, voltage standards, maintenance access, spare-parts availability, and local technical support. A reliable supplier should provide performance data under defined test conditions, not broad marketing promises. That distinction is important.
There is no universal winner. A food processor may prioritize certified oil-free air, while a metal plant may value rugged serviceability and peak-flow capacity. Buyers should challenge assumptions, including their own. A cheaper compressor can become expensive when leaks, heat, poor controls, or neglected dryers remain unresolved. The best choice balances verified efficiency, practical reliability, and long-term operating discipline.
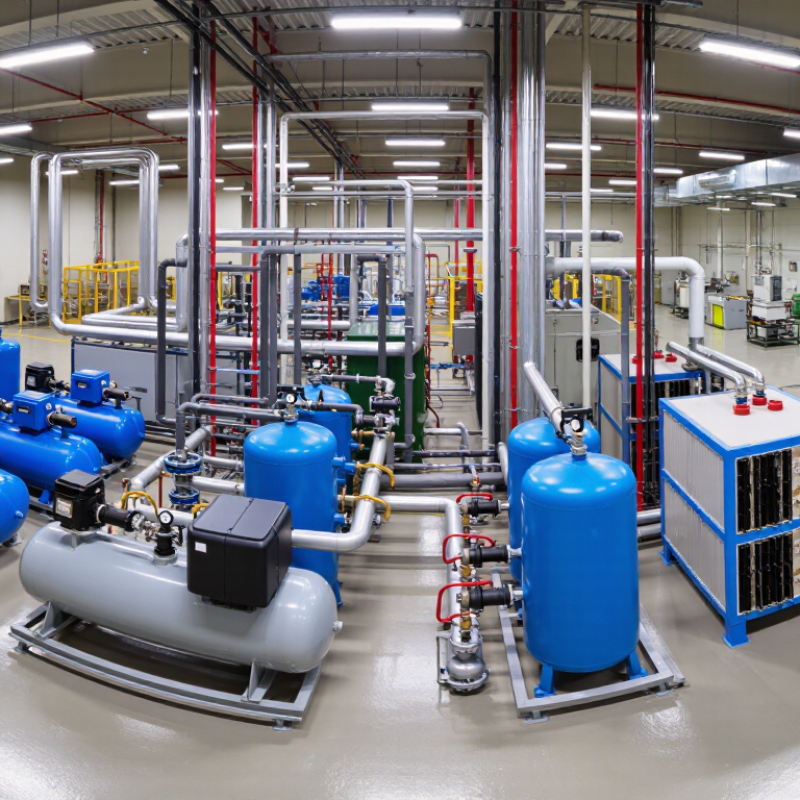
Compressed Air System Types: Reciprocating, Screw, Centrifugal, and Scroll
Compressed air systems differ sharply in output, maintenance, and energy behavior.
Reciprocating compressors suit intermittent demand, workshops, and high-pressure tasks. Their pulsing airflow needs a receiver tank. Noise and vibration can become practical limits.
Rotary screw compressors provide steady airflow for manufacturing lines.
Variable-speed models can reduce unloading losses when demand changes.
The U.S. Department of Energy’s Compressed Air Sourcebook reports that compressed air can consume
10–15% of industrial electricity.
Leaks may waste
20–30% of compressor output.
That makes pipework, pressure settings, and leak surveys as important as compressor selection.
Small leaks sound harmless.
Centrifugal compressors serve large facilities with continuous, stable demand.
They deliver oil-free air and high volume, but poor part-load operation can raise costs.
Scroll compressors offer quiet, clean air for laboratories, medical facilities, and light production.
Their capacity is usually more limited.
ISO 11011 energy assessments recommend measuring supply, transmission, and end-use performance, not just nameplate efficiency.
Buyers should compare duty cycles, required pressure, air quality, ambient temperature, and maintenance access.
A perfectly sized machine can still waste energy when controls or demand patterns are misunderstood.
That weakness deserves review.
Capacity Planning: Match FAD, Pressure, and Duty Cycle at 7–10 bar
Selecting a compressed air system starts with real demand, not the largest nameplate. Free Air Delivery, or FAD, must cover tools, valves, cleaning points, and process losses. Measure demand at the actual operating pressure, usually 7–10 bar.
A workshop may need 18 m³/min at 8 bar, but its compressor should not run continuously at maximum output. Record peak demand, average demand, and idle periods over several shifts. Duty cycle matters. A 70% loaded cycle requires different capacity planning than a machine running nearly nonstop.
Keep a safety margin, but do not inflate it blindly. Ten to fifteen percent may suit stable production, while irregular expansion plans may justify more. Excess capacity can increase cycling, energy use, and maintenance. Too little capacity causes pressure drops at distant outlets. Check pipe length, filters, dryers, and receiver volume. These details quietly reduce usable FAD.
Field readings are valuable. A pressure gauge near the compressor can look healthy while a tool receives only 6.8 bar. Test during peak production, with warm equipment and dirty filters included. Conditions change. Air density falls at high altitude, and hot intake air reduces delivered mass. A spreadsheet can still lie. Recheck the assumptions before approving the system.
Top Compressed Air Systems for Global Buyers - Capacity Planning: Match FAD, Pressure, and Duty Cycle at 7–10 bar
| System Class |
Typical Motor Range |
Rated FAD at 7 bar |
Rated FAD at 10 bar |
Recommended Duty Cycle |
Typical Receiver Size |
Best-Fit Applications |
Planning Guidance |
| Compact Workshop |
2.2–5.5 kW |
0.25–0.65 m³/min |
0.18–0.50 m³/min |
Up to 50% |
100–300 L |
Small workshops, maintenance tools, intermittent blowing |
Allow 20–30% spare FAD for leakage, peak demand, and pressure drop. |
| Light Industrial |
7.5–15 kW |
0.90–1.80 m³/min |
0.70–1.45 m³/min |
50–75% |
300–750 L |
Assembly, packaging, CNC auxiliaries, pneumatic controls |
Select FAD from measured average demand plus the largest simultaneous peak load. |
| General Manufacturing |
18.5–37 kW |
2.20–4.60 m³/min |
1.75–3.70 m³/min |
70–90% |
750–2,000 L |
Metalworking, textiles, food processing, automated production lines |
At 10 bar, expect lower FAD and higher specific energy than at 7 bar. |
| Heavy Industrial |
45–75 kW |
5.40–9.20 m³/min |
4.35–7.40 m³/min |
80–100% |
2,000–5,000 L |
Continuous production, heavy pneumatic machinery, process air |
Consider two compressors for N+1 capacity, maintenance flexibility, and peak-load control. |
| Large Plant Utility |
90–160 kW |
10.80–20.50 m³/min |
8.70–16.50 m³/min |
90–100% |
5,000–10,000 L |
Large factories, centralized air networks, multiple production halls |
Use demand logging and pressure-band control before finalizing total installed capacity. |
Technical note: FAD values are planning ranges expressed in m³/min at standard reference conditions. Actual delivered flow depends on inlet conditions, compressor technology, motor frequency, cooling conditions, altitude, and the applicable test standard. Final selection should be based on measured demand, required point-of-use pressure, pressure losses, leakage allowance, and the compressor’s published performance curve.
Air Quality Selection: Apply ISO 8573-1 Classes for Oil, Water, and Particles
For global buyers, air quality deserves specification before compressor capacity. ISO 8573-1:2010 classifies compressed air by particles, water, and oil. Its notation is particles:water:oil, such as Class 2:4:1. Lower numbers generally require stricter control. Class 0 is not “zero.” It means the user defines tighter limits than the standard’s listed classes.
Selection should start at the point of use. A CNC spindle may need dry, low-oil air. A pneumatic cylinder may tolerate more moisture. ISO 8573-1 separates limits for particles, pressure dew point, and total oil. Do not choose filters from flow ratings alone. Check pressure loss, temperature, oil vapor, and sampling conditions.
The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that leaks can waste 20–30% of compressor output. That loss is easy to miss.
Independent testing remains important. Sample air after installation, during peak demand, and near sensitive equipment. The U.S. Department of Energy’s Motor Systems Sourcebook estimates motor-driven systems consume about 68% of U.S. manufacturing electricity. Compressed air is only one part, but inefficient treatment still adds load. My field lesson is imperfect: clean air at the dryer outlet can hide wet downstream hoses. Recheck the actual tool connection. Record the ISO class, test method, dew point, oil result, and maintenance interval in the purchasing specification. Expect the first specification to need revision.
Global Buyer Checklist: Verify ISO 1217 Testing, CE/UL Marks, and Service Support
Top Compressed Air Systems for Global Buyers
A reliable purchase starts with test evidence, not catalog promises. Request an ISO 1217 acceptance-test report for the exact compressor model. Check delivered flow, input power, pressure, and specific energy. The report should identify test conditions and measurement uncertainty. Small details matter.
The U.S. Department of Energy’s Improving Compressed Air System Performance sourcebook reports that leaks commonly waste 20–30% of compressor output. Ask suppliers to explain leak-control support, monitoring tools, and commissioning procedures. The International Energy Agency reports that electric motor systems consume roughly half of global electricity. Efficient compressors deserve serious scrutiny. Still, laboratory efficiency may not match a dusty factory floor. That gap is easy to underestimate.
Confirm that CE documentation applies to the supplied configuration and destination market. A CE mark indicates conformity with applicable European requirements; it is not a universal performance certificate. For North American projects, verify the relevant UL certification and product scope. Ask for certificate numbers, technical files, and renewal status. Do not accept a logo alone. Service support needs equal attention. Confirm local technicians, spare-parts availability, response times, training, and warranty exclusions. A written service plan is better than a cheerful promise. I would also request references from facilities with similar humidity, voltage, and operating hours. Sometimes, even experienced buyers overlook installation conditions.